Worm Gear hobbing machines are specialized machine tools used to manufacture worm gears and worm wheels with high accuracy and efficiency. Worm gears are widely used in mechanical transmission systems because they offer a large transmission ratio, smooth operation, and the ability to transmit motion between non-parallel, non-intersecting shafts. The design and manufacturing process of a worm gear hobbing machine are crucial to achieving the precision required in modern industrial applications such as automotive systems, machine tools, elevators, conveyors, and precision reducers.
1. Introduction to Worm Gear Hobbing
Hobbing is a machining process in which a rotating cutting tool, called a hob, continuously cuts teeth into a workpiece. In the case of worm gear manufacturing, the machine must accurately coordinate the rotation of the hob and the workpiece so that the generated tooth profile matches the required worm geometry. Unlike simple spur gear cutting, worm gear hobbing requires more complex motion control, rigid structural support, and high positioning accuracy. Therefore, the design of the machine must consider mechanical stiffness, synchronization accuracy, vibration resistance, and thermal stability.
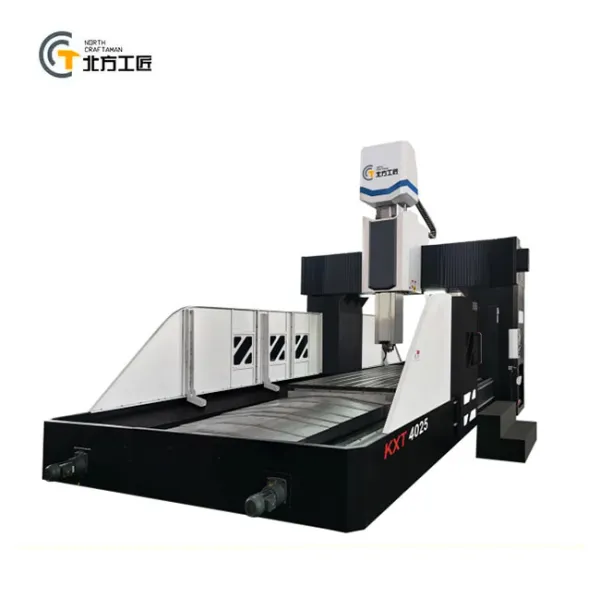
A worm gear hobbing machine generally includes a base, column, spindle system, worktable, feed mechanism, drive system, control system, and cooling/lubrication system. These components work together to ensure efficient cutting and precise tooth formation.
2. Design Requirements
The design of a worm gear hobbing machine begins with defining its functional requirements. The first requirement is accuracy. Since worm gears are often used in transmission systems where backlash and pitch errors can affect performance, the machine must maintain very small errors in indexing, feed, and tool positioning.
The second requirement is rigidity. During hobbing, cutting forces act on both the hob and the workpiece. If the machine frame or spindle system lacks stiffness, vibration and deformation may occur, reducing surface quality and dimensional accuracy. Thus, the machine structure should be designed with high static and dynamic rigidity.
The third requirement is synchronization. The hob and workpiece must rotate in a precise relationship determined by the gear ratio. This is often achieved through a mechanical gear train in traditional machines or through electronic synchronization in modern CNC machines.
The fourth requirement is versatility. The machine should be capable of machining worm gears of different modules, lead angles, pitch diameters, and helix directions. Adjustable fixtures and programmable control systems improve flexibility.
Finally, the machine should be designed for efficiency, ease of operation, maintenance convenience, and long service life.
3. Main Structural Components
The base or bed is the foundation of the machine. It supports all other components and must have excellent vibration damping properties. Cast iron is often used because of its strength and damping capability. The column or frame supports the spindle housing and feed mechanisms, ensuring stable tool movement.
The spindle system is one of the most critical parts. The hob spindle must rotate at high speed with minimal runout, while the workpiece spindle must maintain accurate indexing. High-precision bearings are typically used to improve stability and reduce wear.
The worktable holds the worm gear blank and provides rotational motion during cutting. It must be designed to withstand cutting loads and maintain accurate positioning. In many machines, the table can also be inclined to accommodate different worm gear geometries.
The feed mechanism controls the relative motion between the hob and workpiece. In traditional designs, feeds are transmitted mechanically through lead screws and gears. In CNC machines, feed motion is controlled by servo motors and digital controllers, allowing better precision and automation.
The drive system supplies power to the spindle and feed axes. Modern machines often use separate motors for each axis, which simplifies control and improves responsiveness. The cooling and lubrication system is also essential, as it removes heat, reduces friction, and prolongs tool life.
4. Design Process
The design process starts with requirement analysis and machine specification. Engineers define the maximum workpiece size, module range, cutting speed, production capacity, and accuracy level. Based on these requirements, they determine the overall layout and motion scheme.
Next, the kinematic design is carried out. This involves calculating the relationship between hob rotation and workpiece rotation to ensure correct tooth generation. The feed ratios, spindle speeds, and tool paths are established at this stage.
Structural design follows. Engineers use CAD and finite element analysis to optimize the machine frame, spindle housing, table support, and other load-bearing parts. The goal is to reduce deformation and vibration while keeping the structure compact and practical.
Then comes the transmission design. The machine may use gears, belts, ball screws, or servo drives depending on the type. The transmission system must be selected for high efficiency, low backlash, and long-term stability.
After that, the control system is designed. In modern CNC worm gear hobbing machines, PLCs, servo drives, and industrial computers are used to control all motion axes. Programming functions allow operators to input gear parameters and automatically generate the machining cycle.
Finally, the design is tested through simulation and prototype trials. Any issues in accuracy, stiffness, or heat generation are corrected before mass production begins.
5. Manufacturing Process
The manufacturing of a worm gear hobbing machine begins with material selection. The bed and major structural parts are usually made of high-quality cast iron or steel. These materials are chosen for their strength, wear resistance, and damping characteristics.
The next step is rough machining. Large castings are processed by milling, turning, drilling, and boring to remove excess material and create reference surfaces. This stage establishes the basic geometry of the parts.
Heat treatment may be applied to certain components such as gears, shafts, and spindles to improve hardness, wear resistance, and fatigue strength. Stress relief treatment is also important for castings to minimize distortion during later machining.
Precision machining is then performed. Critical parts such as spindle bores, guideways, ball screw seats, and locating surfaces are machined to very tight tolerances. Surface grinding, honing, and lapping may be used to achieve the required finish and accuracy.
After machining, components are assembled. During assembly, alignment is carefully checked to ensure proper geometry between the hob spindle, worktable, and feed axes. Bearings, motors, couplings, and drive elements are installed and adjusted.
The machine then undergoes inspection and testing. Geometric accuracy, spindle runout, feed precision, noise level, and vibration are measured. Test cutting is carried out to verify the quality of worm gear production. If errors are found, adjustments are made before delivery.
6. Modern Trends
With the development of automation and digital manufacturing, worm gear hobbing machines are increasingly equipped with CNC systems, automatic tool changers, and online monitoring devices. These improvements enhance productivity, reduce operator dependence, and improve machining consistency. Intelligent control systems can also compensate for thermal drift and tool wear, further improving precision.
Another trend is the use of advanced materials and lightweight structures to reduce energy consumption and improve dynamic performance. In addition, digital twin technology and simulation-based design help engineers optimize machine performance before physical prototyping.
7. Conclusion
The design and manufacturing process of a worm gear hobbing machine involves a combination of mechanical engineering, precision manufacturing, control technology, and system integration. To produce high-quality worm gears, the machine must provide accuracy, rigidity, synchronization, and reliability. From conceptual design and kinematic analysis to structural optimization, precision machining, assembly, and testing, every step directly affects the final performance of the machine. As CNC technology and intelligent manufacturing continue to advance, worm gear hobbing machines will become more efficient, more precise, and more adaptable to the needs of modern industry.

 Pусский
 العربية


